Industrial Tube Blank Cutting
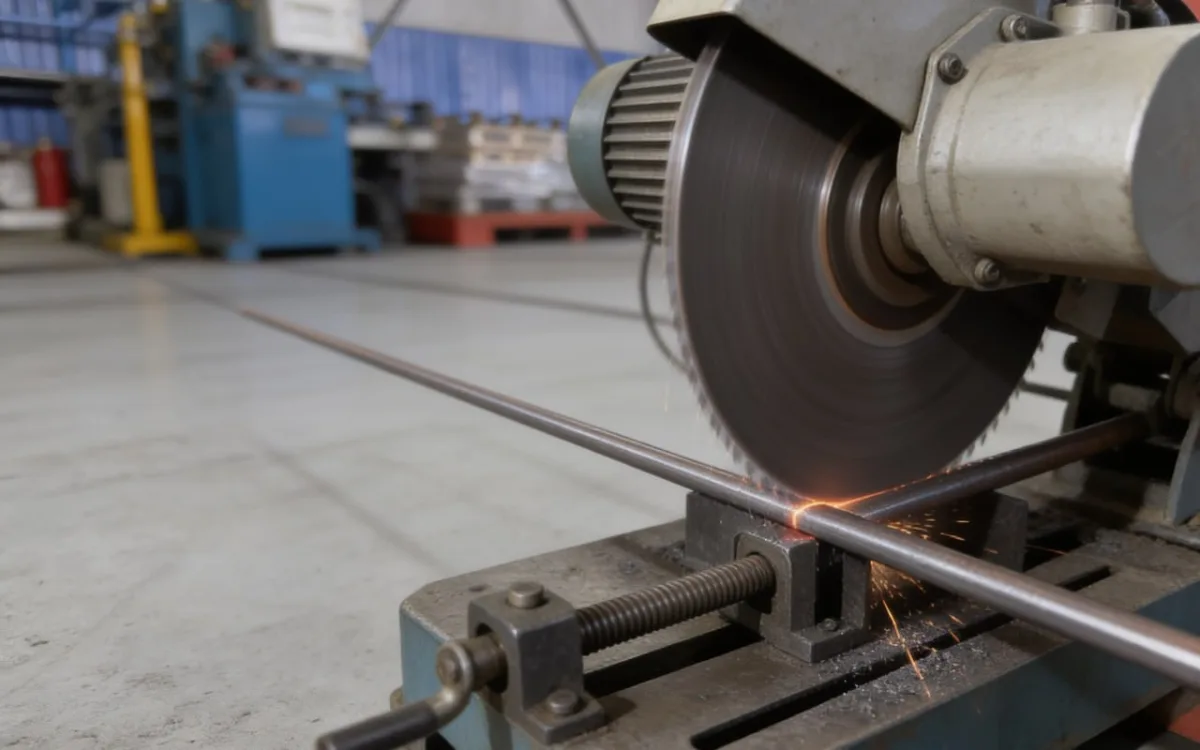
Industrial cutting of tube blanks on cut-off saws with repeatable batch length.
We cut round and profile tubes into blanks for furniture, metal structures, retail equipment and other serial products. Before production, we confirm the tube type, blank length, tolerances, quantity and end-face requirements.
Need a Production Assessment?
Send a drawing, 3D model, sample or short description. We will clarify the parameters and advise on the next steps.
Tube blank cutting
Industrial cutting of tubes into measured blanks
AMF cuts tubes into blanks on industrial cut-off saws. Round and profiled tubes are divided into parts of an agreed length for serial welding, assembly, furniture, retail equipment and metal structures. AMF tube or customer material can be used. For a quotation, send the length schedule, section, wall thickness, quantity and end requirements.
- Round and profiled tubes.
- Serial batches of measured parts.
- Agreed tolerances and end requirements.
- AMF material or customer-supplied tube.
- Marking and order preparation by item after agreement.
Send the blank schedule or call +38 (067) 223-11-22.
Serial tube blank cutting
In serial production, the length of every blank affects the assembly rate. If dimensions vary, parts must be adjusted and repositioned in the fixture.
Industrial tube cutting makes this a separate controlled stage. Before launch, the source tube, each item length, quantity, tolerance, end, marking and packaging requirements are agreed. The batch is then cut to the schedule and prepared so it can enter the next operation without repeated sorting.
The service suits one repeated length or a set of items from common stock lengths. The cutting plan links every part to its order item.
Tubes that can be cut
AMF works with round electric-welded and profiled tube. Section, wall and length ranges are checked against the order and machine capabilities. The technologist assesses the actual tube, required cut and batch conditions.
| Tube type | What to include in the schedule | What production checks |
|---|---|---|
| Round electric-welded | Outside diameter, wall thickness, length and quantity | Secure clamping, cutting mode and end requirements |
| Square profiled | Side size, wall thickness, length and quantity | Profile orientation, clamping deformation and batch repeatability |
| Rectangular profiled | Width, height, wall thickness and installation direction | Machine position, cutting plan and length control |
| Oval or flat-oval | Full section dimensions, wall thickness and a sample or drawing | Profile holding and geometry retention |
| Customer-supplied tube | All dimensions plus grade, condition and source-stock length | Material compatibility, incoming geometry and accounting procedure |
For a non-standard section, attach a dimensioned drawing or photograph. Feasibility is confirmed after parameter review.
Cutting on cut-off saws
Saw cutting mechanically divides tube into straight measured parts. The tool passes through the profile walls and the cutting mode is selected for the material, section and thickness. The result is an agreed batch length and controlled end condition.
Before a run, the saw is set for the item. Tube is clamped, fed to the set dimension and cut. Multiple lengths are combined into a cutting plan that accounts for source stock and process remnants.
A cut-off saw is used for straight division to length. Holes, slots and shaped joints require programmed laser processing.
How an order is processed
The production route starts with the schedule. Accurate items simplify material calculation.
01
Task receipt
We accept a drawing, cutting schedule or table with dimensions and quantities.
02
Tube review
We check section shape, wall thickness, material grade, source length and stock condition.
03
Result agreement
We record length, tolerance, angle and end requirements, deburring, marking and order-preparation needs.
05
Cutting-plan preparation
Items are allocated across source lengths with process allowance and remnants considered.
06
Serial cutting
Parts are cut in the agreed sequence and separated by item.
07
Inspection and packaging
We check length and ends, count blanks, apply agreed marking and prepare the batch.
If parts go directly to welding, bending or assembly, state this because the next operation determines end, burr and packaging requirements.
AMF tube or customer material
When electric-welded tube is needed with the blanks, AMF can produce a round or profiled section from cold-rolled steel and send it directly to cutting. This creates one agreed route: raw material, tube, measured part and order preparation.
The standalone service suits companies that already have tube. Before delivering customer material, provide:
- section shape and size, and wall thickness;
- material grade and condition;
- length and quantity of source stock;
- existing marking and batch separation;
- finished-parts list and permitted remnants;
- accounting, remnant-return and packaging requirements.
Different grades and batches should be supplied separately with clear marking.
Batch length and quality control
Permitted deviation is agreed before quotation according to the section, part length, material and downstream operation. One universal tolerance is not promised for all tubes.
Batch inspection may include:
- each scheduled item length;
- squareness or agreed end angle;
- edge condition and burr;
- profile-shape retention after clamping;
- part count for each item;
- marking and separation of sets.
Sampling or 100% inspection is determined by the order requirements. For fixture assembly, attach the control dimensions from the drawing.
Deburring is agreed separately because the end condition depends on material, wall, cutting mode and the next operation.
When laser tube cutting is required
Saw cutting is the primary choice when a tube must be divided straight into measured blanks. It suits serial cutting to length and preparation for welding, assembly or further machining.
Laser tube cutting serves another purpose: it produces holes, slots, shaped contours and complex joining lines from a digital program. AMF can prepare a program for an individual order after checking the drawing and input format. If parts need both a set length and complex contours, describe both operations in one technical specification.
Where finished blanks are used
Measured tube parts are used where assembly repeats from batch to batch.
- Furniture frames. Legs, rails, supports and frame elements before welding or fastening.
- Retail equipment. Uprights, shelving, display structures and serial modules.
- Metal structures. Frames, supports, guards and welded-assembly elements.
- Mechanical engineering. Parts that proceed to drilling, bending, welding or machining.
- Kitted orders. Sets of different tube lengths separated by item, product or assembly operation.
State the specific part in the request and attach a drawing with length, tolerance and weld zone.
What determines the cutting price
Cost is not based only on the number of cuts. Factors include:
- tube type, size and material;
- wall thickness and source-stock length;
- finished-part lengths and quantities;
- number of schedule items;
- required tolerance and end angle;
- deburring and additional operations;
- marking, kitting and packaging;
- AMF tube or customer material;
- batch volume and requested timing.
With multiple lengths, the cutting plan affects material use and the final quotation.
What to send for a quotation
Prepare a schedule or drawing showing:
- section shape and size;
- wall thickness and steel grade;
- each blank length;
- quantity for each item;
- tolerance and end requirements;
- AMF or customer material;
- deburring requirement;
- marking, kitting and packaging;
- delivery destination and requested completion date.
If the blanks will also be laser processed, add a drawing with holes and contours. Send the schedule through the contact form or call +38 (067) 223-11-22.
FAQ
Which tubes does AMF cut into blanks?
We process round electric-welded and profiled tubes. Feasibility for a specific section, wall and length is checked against the order schedule. For oval, flat-oval or non-standard profiles, attach a dimensioned drawing or sample.
What minimum and maximum blank sizes are available?
The range depends on section, wall thickness, clamping method and selected saw. Send the source-tube length and finished-parts list. A technologist will check the limits before quotation.
What length tolerance can be achieved?
Tolerance is agreed individually for the tube and batch. Section, wall, part length, material and end requirements affect the result. State the permitted deviation on the drawing, and AMF will confirm whether the selected equipment can achieve it.
Can identical parts be cut in series?
Yes. Serial tube blanks are the primary purpose of this service. A schedule may contain one length or several items. Quantity, tolerance, inspection, marking and order preparation are agreed before launch.
Can I supply my own tube?
Yes. State the section, wall, grade, stock length and quantity, surface condition and batch marking. Material accounting and return of process remnants must also be agreed in advance.
How does saw cutting differ from laser cutting?
A cut-off saw divides a tube straight into specified lengths. A laser is used when holes, slots, shaped contours or complex programmed joints are also required. The correct process depends on the drawing and result.
Are blanks marked and kitted?
These operations can be included after agreement. State the marking format, item list, number of parts per set and packaging method. Production will confirm the available option and include it in the quotation.
What determines the cutting cost?
Price depends on the tube, number of parts, tolerance, end, marking and packaging requirements. The supply scheme—AMF tube or customer material—is considered separately.
What files are needed for laser-processing quotation?
For saw cutting, a length schedule and section drawing are usually sufficient. Holes, slots and shaped contours require a part drawing; the preferred digital format and any programming work are agreed after technical review.